Project Implementation
- Implementation Period: January – April 2024
- Recipient: Pulp and Paper Industry Facility
- Location: Quay wall designated for unloading long-length timber from railcars, river vessels and trailers.
GTAKE’s project scope covered electrical system modernization, drive panel manufacturing, control system replacement, motor replacement, installation supervision and commissioning.
The implementation process included electrical documentation development, equipment manufacturing, on-site installation support, system commissioning and final testing.
Drive Power
The upgraded crane included multiple drive applications with different power requirements:
- Main Hoist: 250 kW
- Crane Travel: 8 × 15 kW, controlled by 2 frequency inverters, with 4 motor-reducers on each side
- Trolley Travel: 25 kW
The main hoist represents the highest-power drive application in the system, while the crane travel system uses multiple motors that require coordinated control. The trolley travel system uses a separate 25 kW drive application.
This configuration demonstrates the use of crane VFD technology across different motion functions, including hoist drive, crane travel and trolley travel.
Drive System Configuration
The crane modernization required different drive capacities and control functions for the main hoist, crane travel and trolley travel systems.
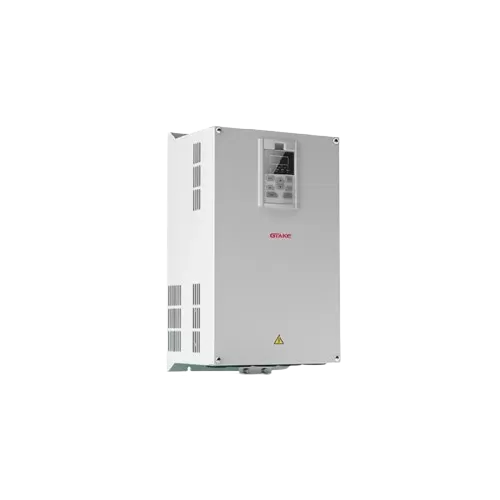
For the main hoist, the GK820 High-performance AC Drive provides advanced motor control functions suitable for demanding lifting applications. GK820 supports V/f control, sensorless vector control and closed-loop vector control, allowing the control method to be selected according to motor and application requirements.
For multi-motor travel applications, drive configuration and motor synchronization should be determined according to the mechanical arrangement, motor ratings, load distribution and control architecture.
Challenges Addressed
The modernization project addressed several challenges associated with the aging crane electrical system:
- The initial equipment had been discontinued, making spare parts and long-term maintenance increasingly difficult.
- The old Simatic S115 controller experienced frequent failures.
- The main hoist motor had broken down and required replacement.
- The aging electrical system required updated documentation and control software.
- The crane required commissioning and testing after the electrical modernization.
Replacing obsolete equipment with a modern AC drive system helped establish a more maintainable electrical architecture for the crane.
Key Accomplishments
- Developed new electrical documentation for the modernized crane system.
- Manufactured new electric drive panels using GTAKE frequency inverters.
- Replaced the old controller and developed custom application software for the updated control system.
- Replaced the 250 kW main hoist motor and associated electrical components.
- Supervised electrical installation and system integration.
- Completed commissioning and functional testing.
- Ensured the modernized crane passed the required tests and returned to operation.
Crane Electrical Modernization Process
The project followed a complete crane retrofit process rather than simply replacing a single frequency inverter. The modernization covered:
Electrical documentation → Drive panel manufacturing → Controller replacement → Motor replacement → Installation → Commissioning → Testing
This integrated approach is important for industrial cranes where the drive, motor, controller, braking system and mechanical equipment need to operate as one coordinated system.
Product Advantages of the GK820-52
The GK820 High-performance AC Drive was selected for the demanding motor-control requirements of the modernized crane system.
- High Starting Torque: GK820 can provide up to 200% starting torque at 0 Hz under closed-loop vector control, supporting high-torque starting conditions when the motor and feedback configuration meet the required conditions.
- Precise Speed and Torque Control: GK820 supports V/f, sensorless vector and closed-loop vector control, providing different levels of speed and torque control according to the application requirements.
- Fast Torque Response: The specified torque response is below 10 ms under applicable sensorless vector control modes and below 5 ms under closed-loop vector control.
- Encoder Feedback: Closed-loop vector control can use encoder feedback for applications requiring higher speed and positioning accuracy.
- Mechanical Brake Control: GK820 includes mechanical brake control functions for compatible lifting and industrial machinery applications.
- Dynamic Braking: Dynamic braking functions can be configured according to the drive model and application requirements.
- Flexible Control: Multiple frequency-setting sources, digital and analog I/O, communication functions and programmable control functions support integration with different industrial control systems.
For crane applications, protection and control functions should be configured according to the complete equipment architecture and applicable safety requirements. Drive functions are one part of the overall crane control and safety system.
Results
In April 2024, the modernized crane successfully completed commissioning and testing and was returned to operation.
The project replaced obsolete electrical equipment, updated the control system, installed modern GTAKE AC drives, replaced the main hoist motor and completed system commissioning.
By April 2024, more than 20 cranes were operating with GTAKE inverters, demonstrating GTAKE’s experience in applying AC drive technology to industrial crane and material-handling applications.